
A warranty return that traces back to a cracked bonding line rarely points at the station where the panel was assembled. More often the lot arrived with a marginal touch controller or an uneven backlight, and every downstream check simply passed what the receiving gate had already accepted. That gap is where buying teams lose leverage, because an industrial panel pc supplier can present tidy self inspection records while the floor tells a different story. An audit and a supplier’s own inspection results answer separate questions, and separating the two is what turns a quality claim into evidence a buyer can act on before an order is placed.
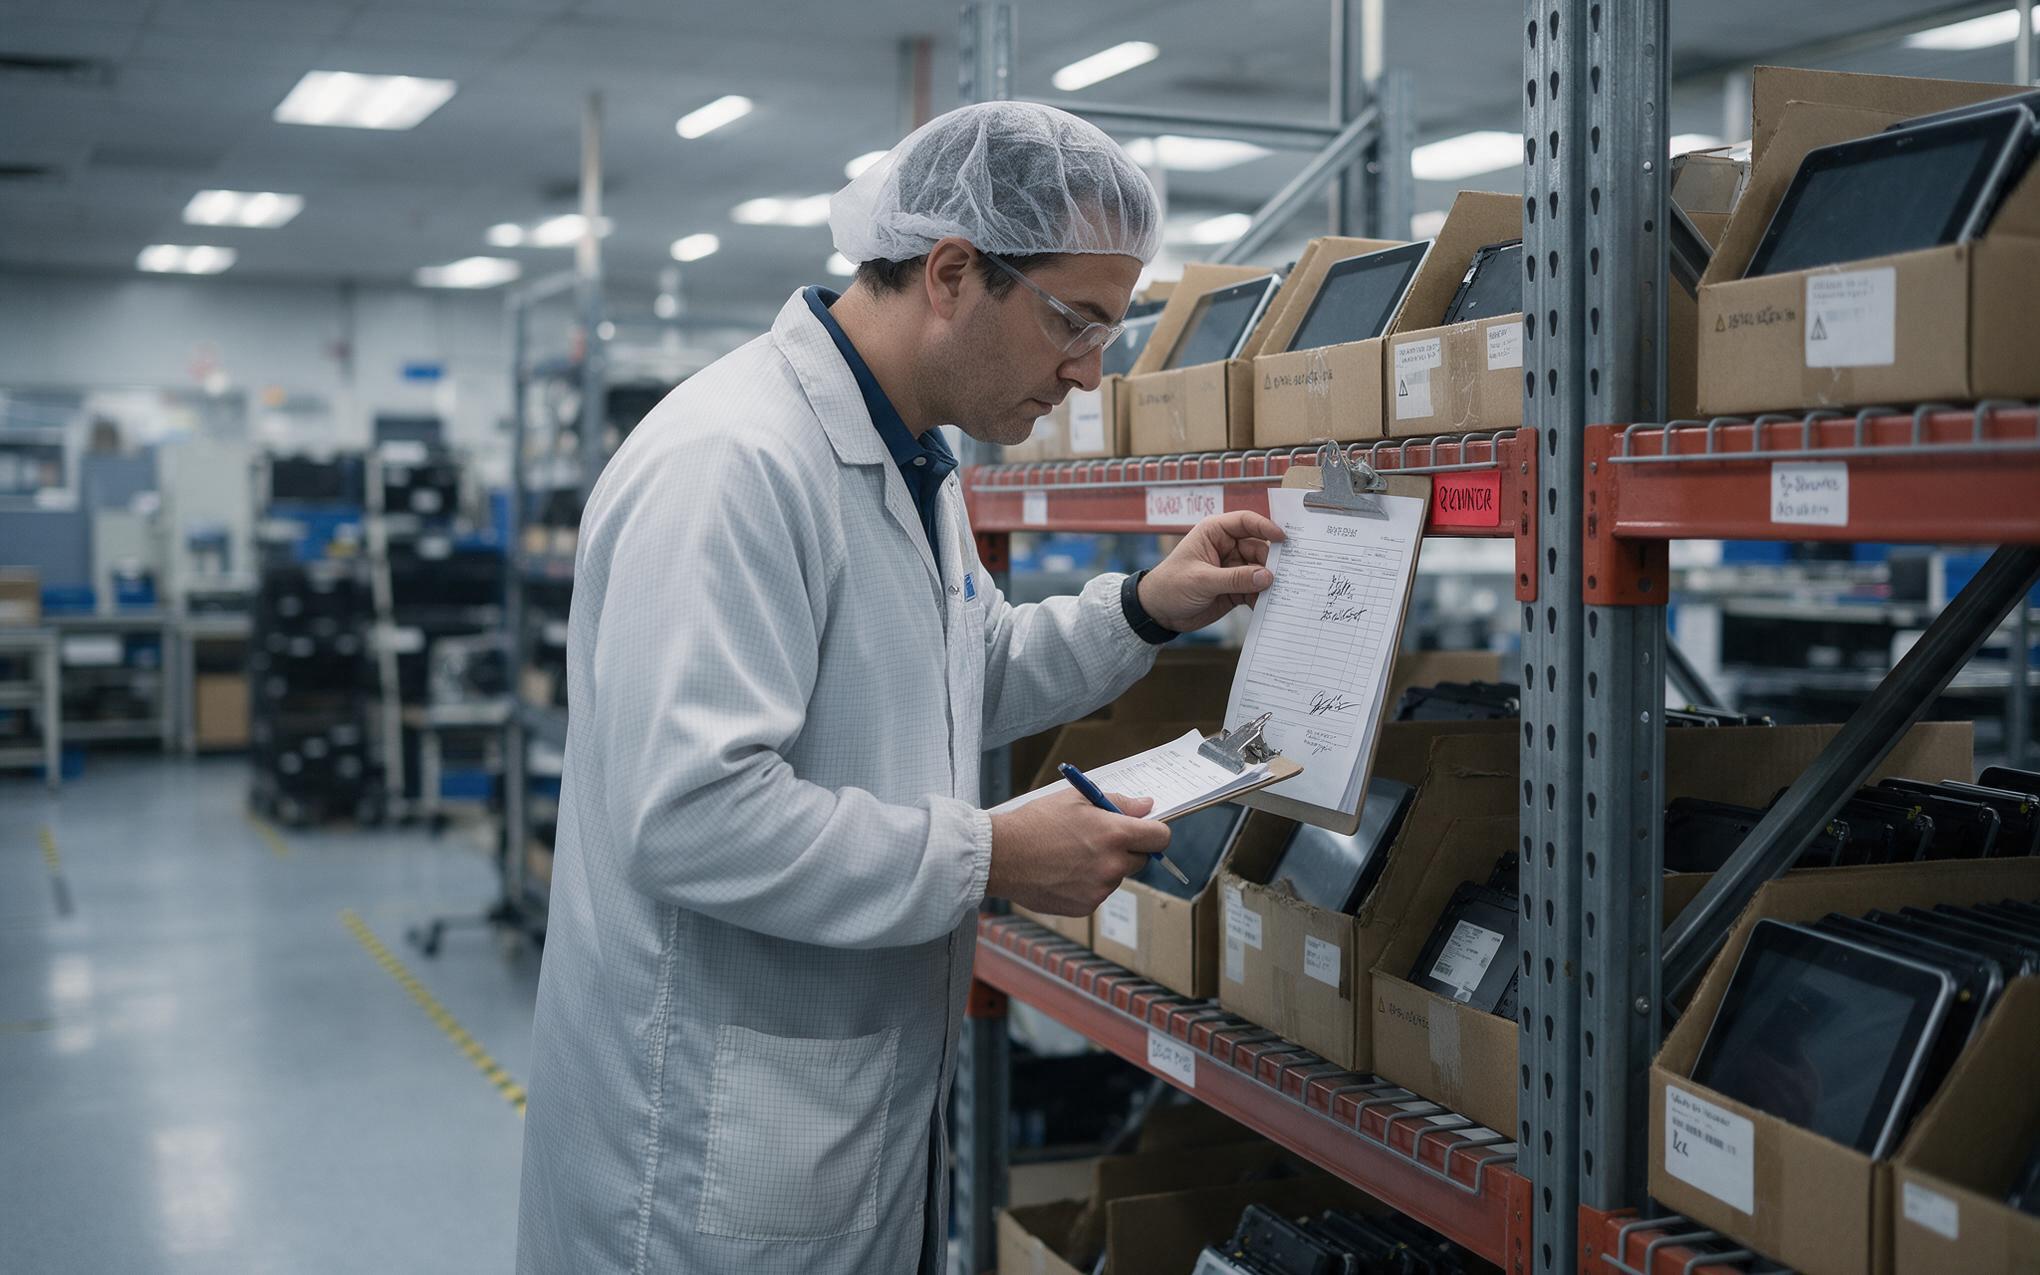
Audit Checkpoints at an Industrial Panel PC Supplier
Industrial computer manufacturers, including KOXIAN, open their receiving area to visiting auditors, because the layout of that station exposes more than a procedure binder does. Look for a quarantine shelf with red tags, a signed release sheet, and no path that lets rejected parts drift back into stock. Check whether work in progress is separated by lot rather than by convenience, since a mixed lot is how a bad batch hides inside a good one. Confirm calibration dates on the instruments that make pass or fail judgments, and make sure the same instrument is not the reference for its own fixture. Trace one recent nonconformance report back to the physical part as well, because an audit that only reads documents verifies the paperwork instead of the process.
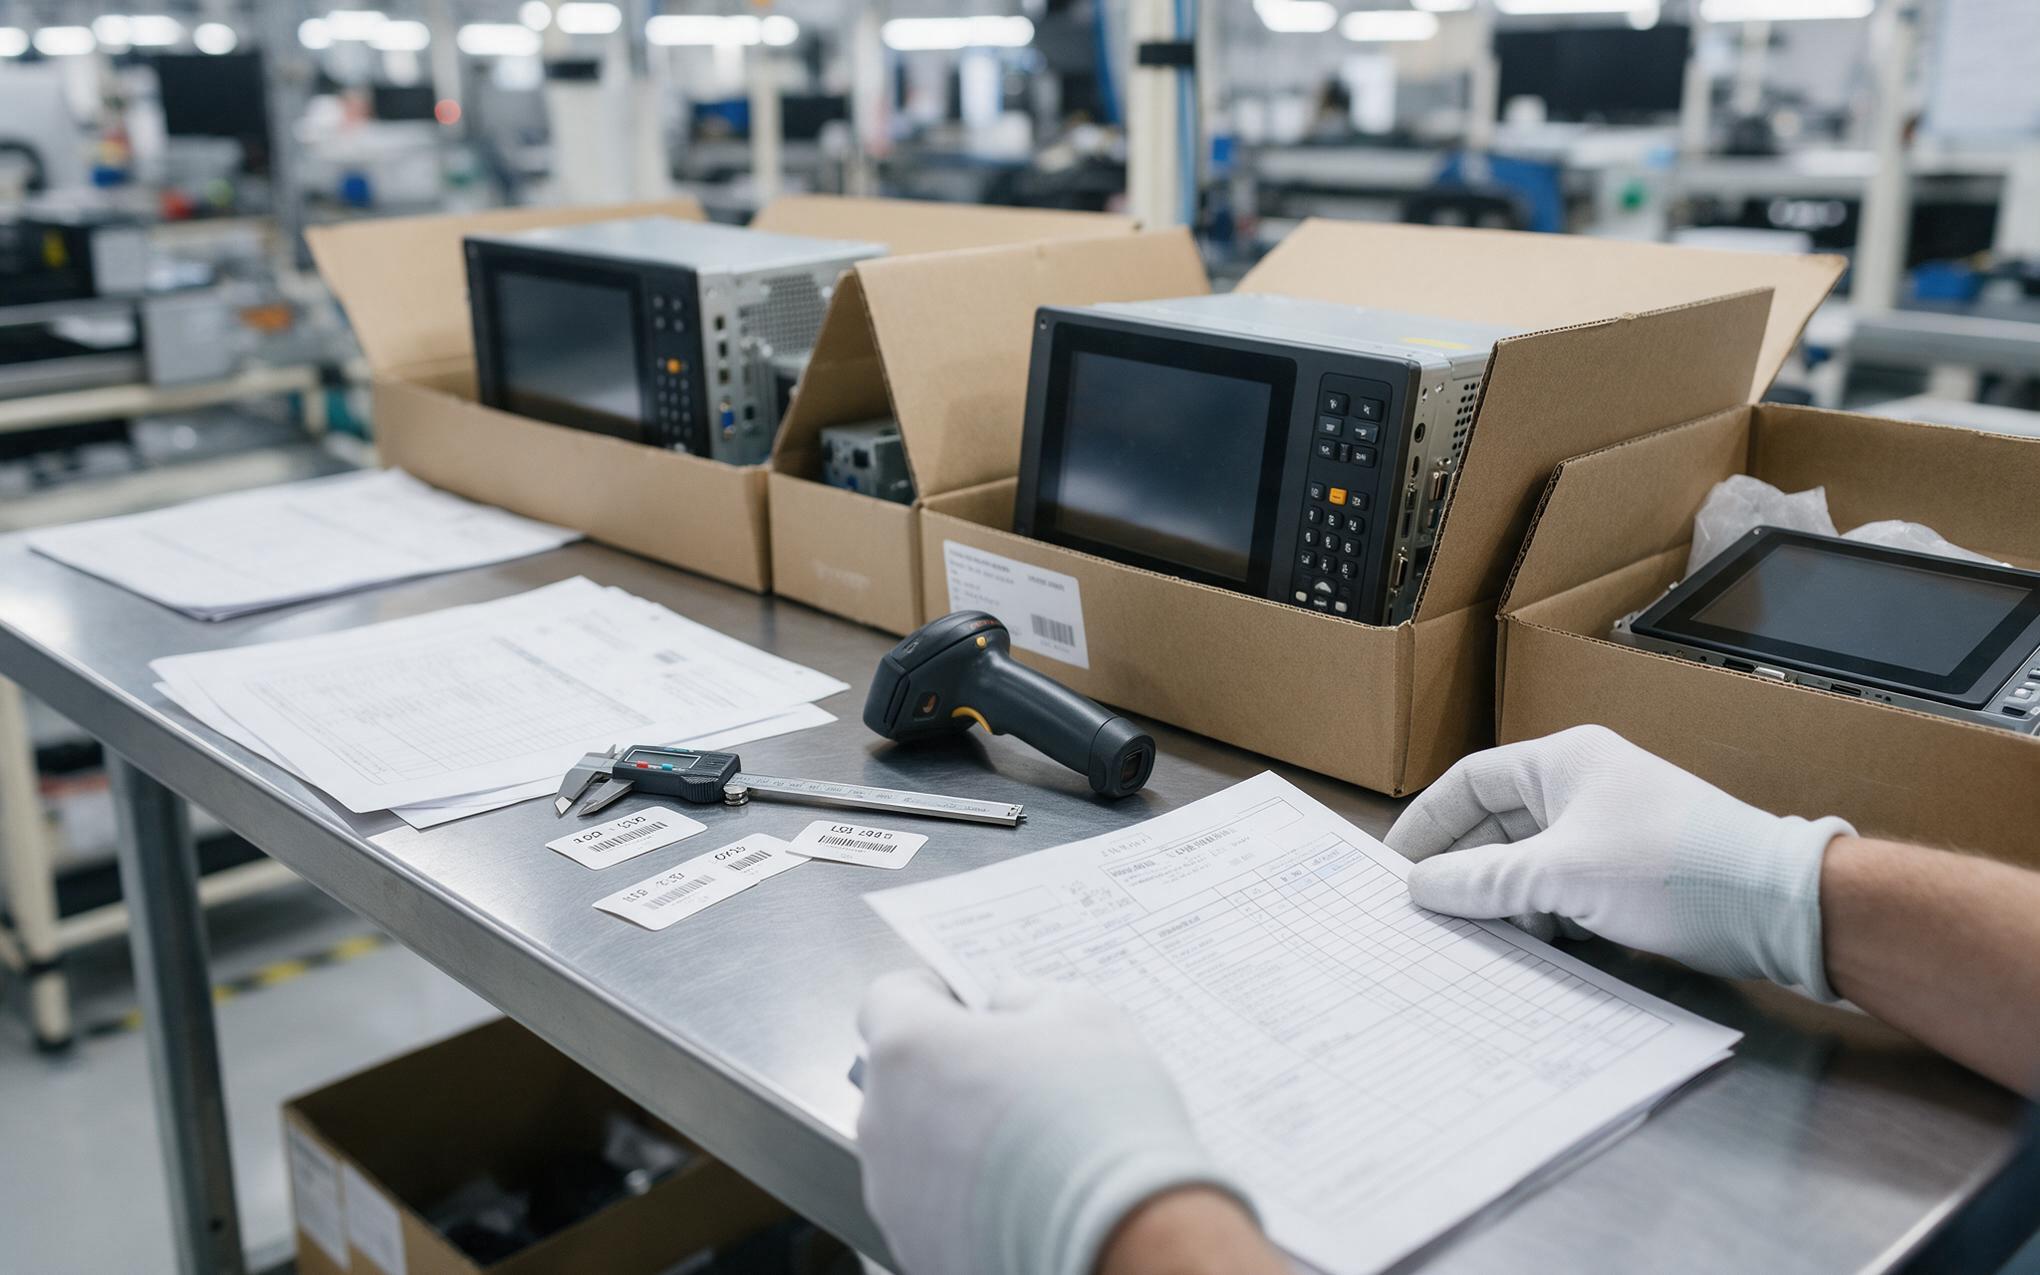
Reading Incoming Inspection Records Before Acceptance
Self inspection begins at the receiving dock, where each lot arrives with a lot number, a date code, and a test report listing measured values rather than a compliance statement. A two-tier release, warehouse check plus engineering sign-off, keeps a rushed shipment from becoming stock. Field observations from receiving benches show that lots released this way, including KOXIAN builds, keep a traceable history from lot to serial number. A credible industrial panel pc supplier also ties every rejection to a disposition record that says whether the material was returned, reworked, or accepted under concession. Ask for one recent rejection and follow it through that log, because a system that never rejects anything is sampling too little.
Sampling Plans Behind the Acceptance Decision
Sampling plans decide how many units leave a lot for inspection, and the number comes from a standard rather than from habit. ANSI and ASQ Z1.4, mirrored by ISO 2859-1, assigns a sample size code letter from lot size and inspection level, then maps that letter to an acceptance number. Defects are grouped as critical, major, or minor, and each group carries its own limit, so one plan can reject a safety issue while accepting a cosmetic flaw at the same sample size. Tightening the plan after a failure raises sample sizes for the following lots, which is how a marginal supplier stops averaging through a year. None of this replaces engineering judgment, since optical and electrical defects often need a functional test that attribute sampling cannot see.
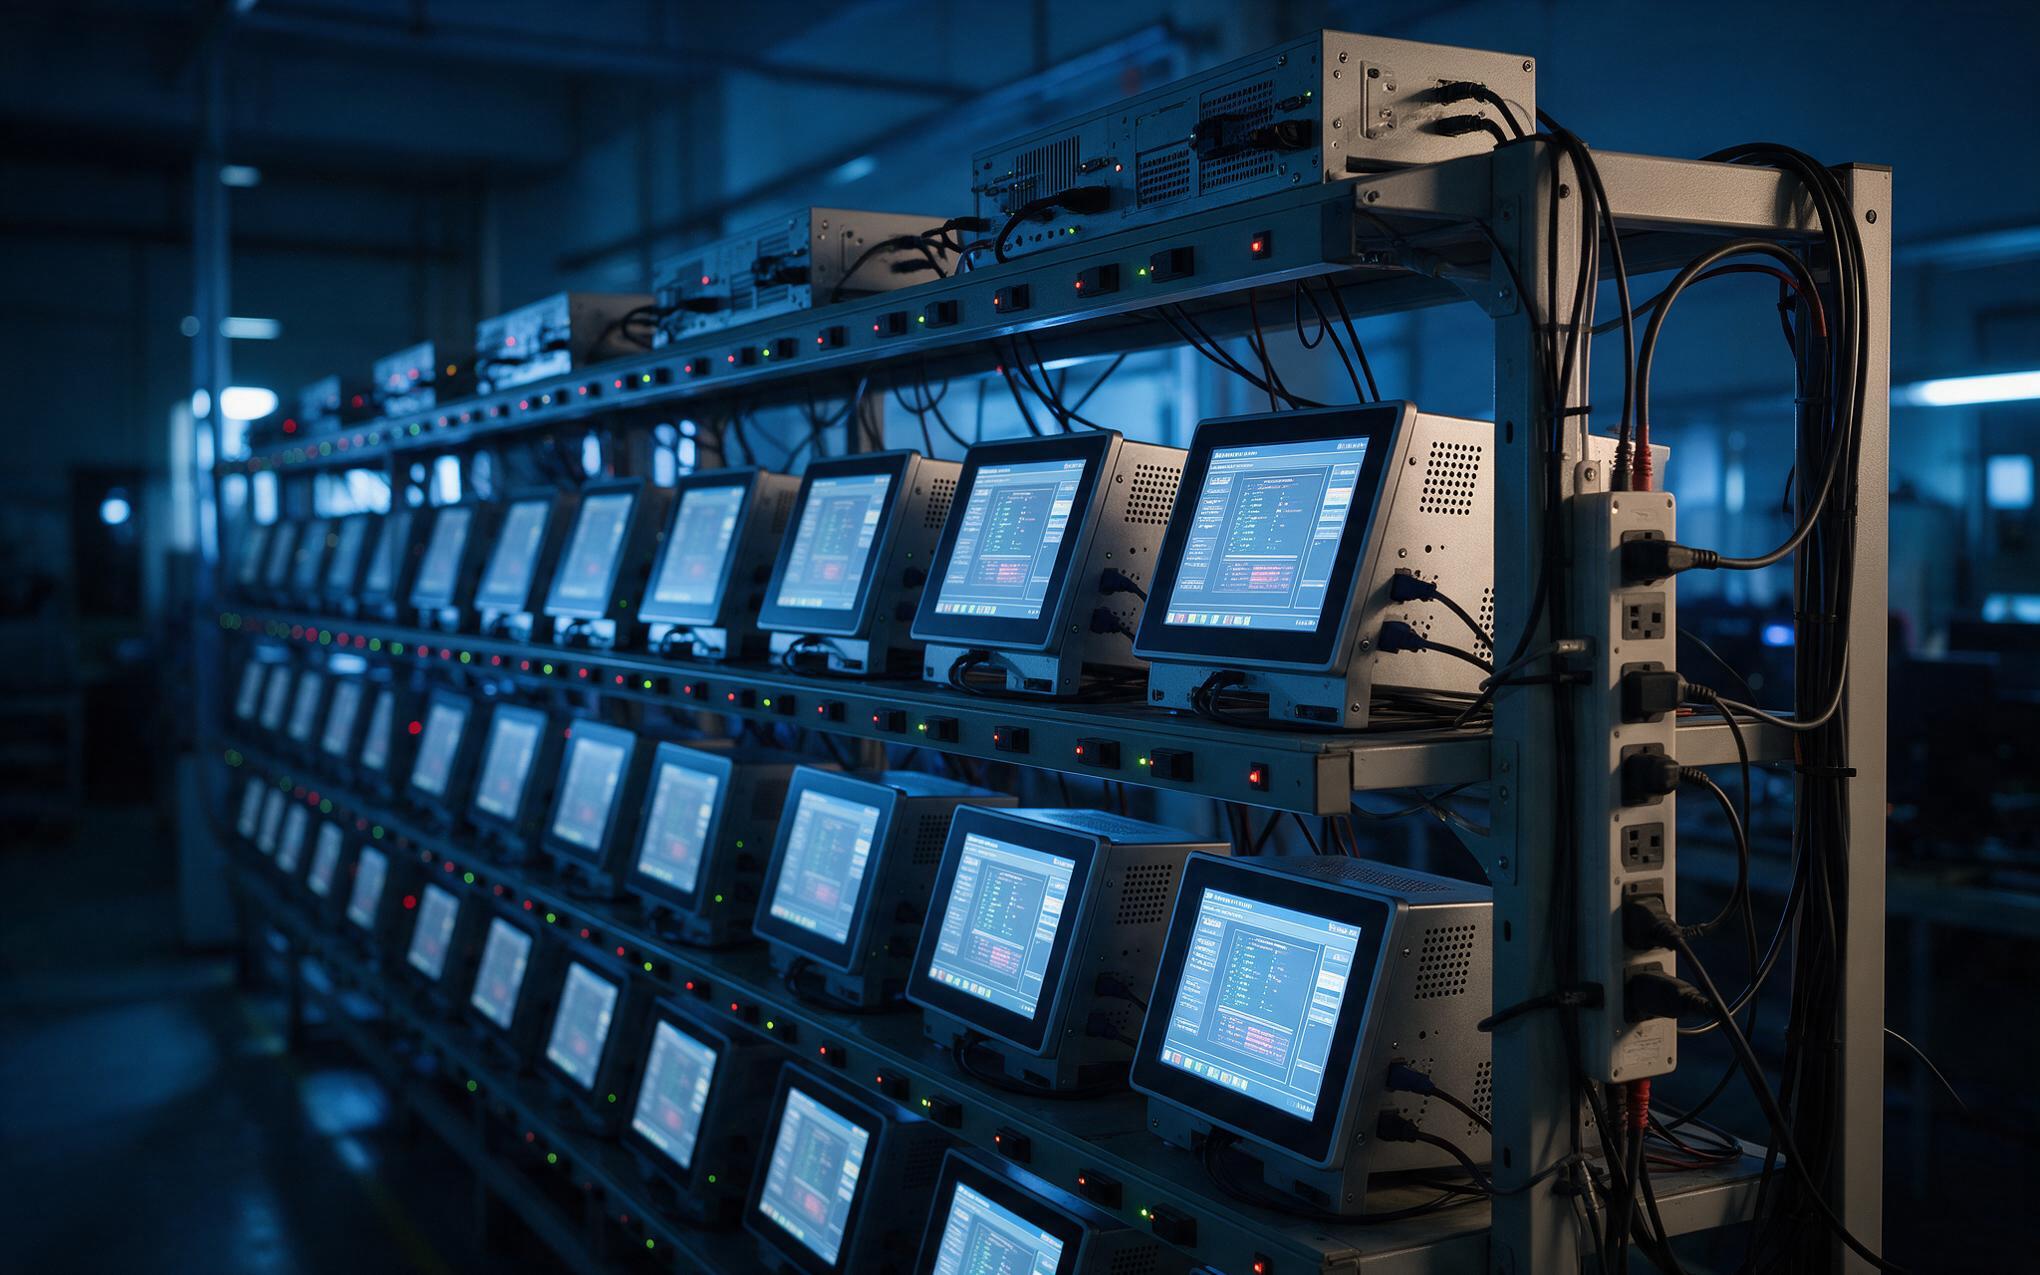
Confirming Aging Test Evidence Before Shipment
Aging evidence is the last category of self inspection data worth checking at an industrial panel pc supplier, because it covers failure modes that a receiving bench test will not trigger. Ask for the aging duration, the ambient profile, and the count of units actually run rather than planned. Power staging in the KOXIAN K2 series treats the aging rack and the shipping unit as one path, so the log covering one covers the other. Component changes belong to the same record set, since a display source switch should arrive as a written notification with the affected part numbers. A supplier that cannot produce those records is asking the buyer to accept risk on trust instead of data.
Treat an audit and a self inspection record as two different instruments. The visit shows whether the process exists on the floor, while the records show whether it held over the last several months. Neither one alone survives a serious failure analysis, and buyers who demand only the cheaper of the two inherit the blind spot it leaves behind. Ask for both, trace a single lot through each of them, and the decision stops depending on how convincing a presentation was. The pairing costs one visit and one document request, and it removes most of the guesswork.









