
A warranty trend appears late every winter, when service tickets from outdoor kiosks and cold docks describe the same defect: a faint crescent of light along the display edge that grows after weekend shutdowns. The returned units share one feature, a fully bonded front assembly made with an industrial panel pc optical bonding process that laminates cover glass and touch sensor directly to the LCD cell. The bond eliminates the internal air gap where condensation and dust collect, but a sealed stack has nowhere to move. When temperatures swing between night idle and daytime operation, every layer changes length, and that difference loads the adhesive. Calling this a one-off seal failure hides the mechanism, which lives in the coefficients of thermal expansion.
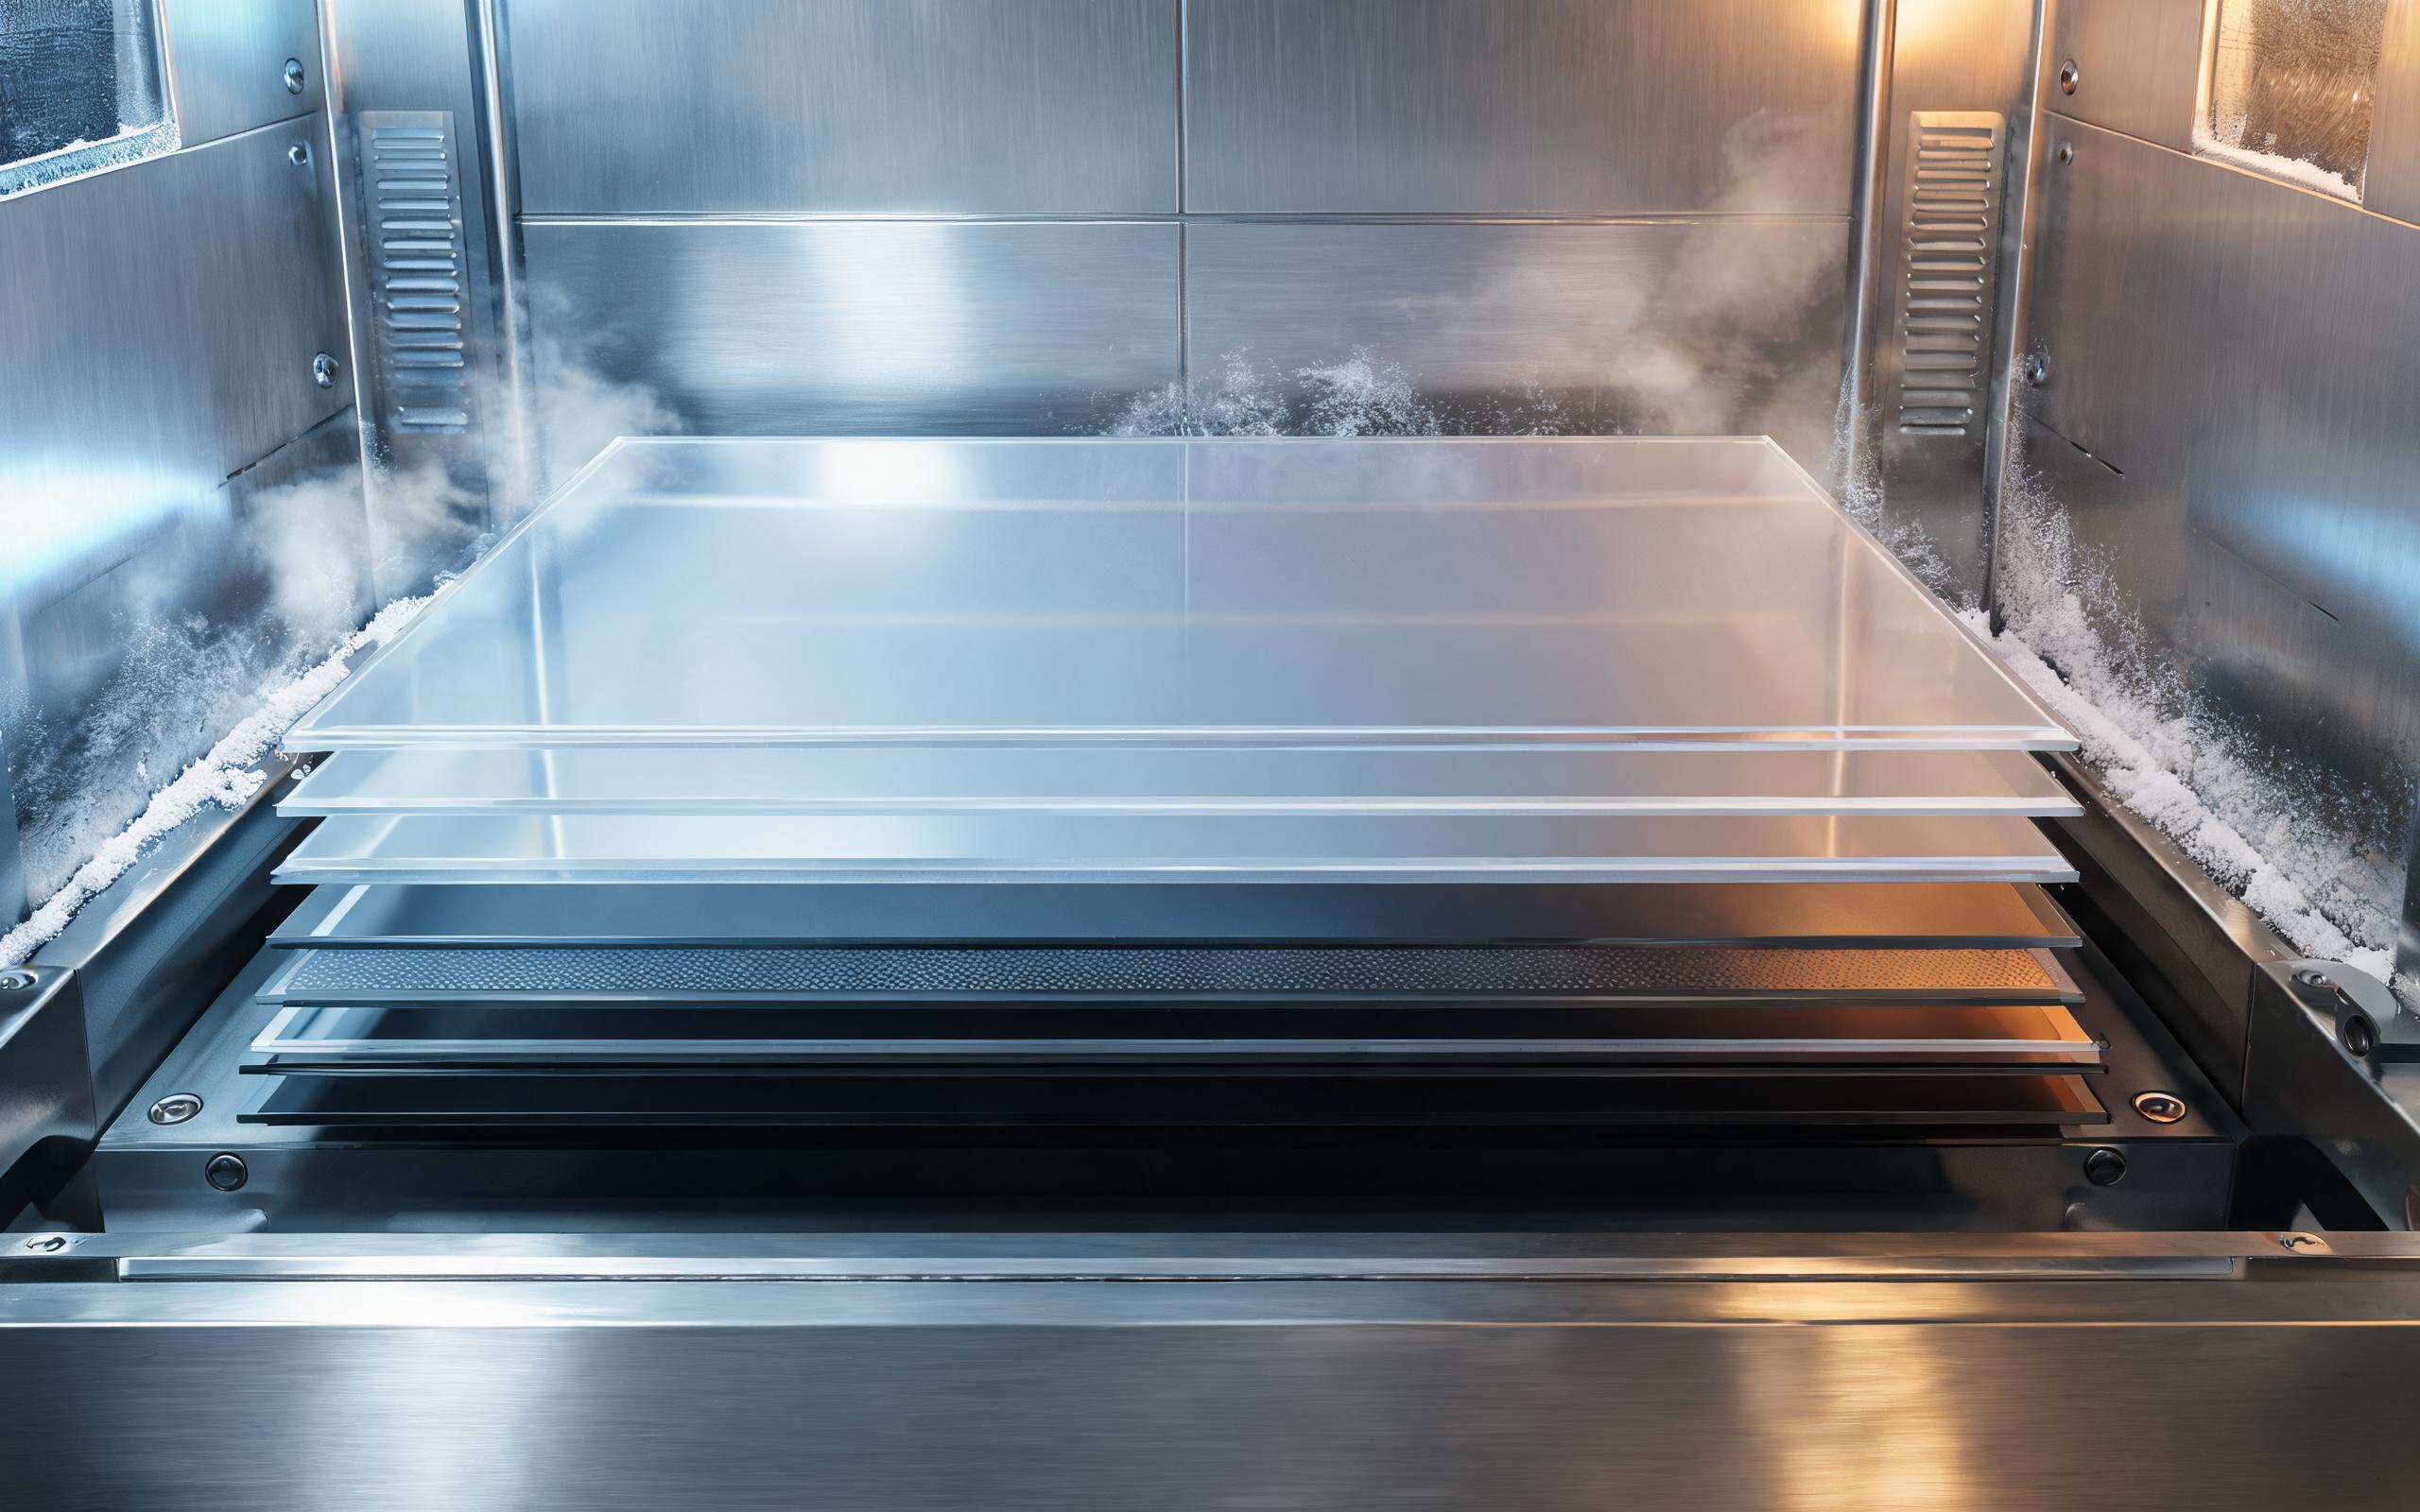
Thermal Expansion Mismatch Across the Bonded Stack
To manage differential strain across the stack, industrial panel pc optical bonding manufacturers, including KOXIAN, select adhesives against a table of coefficients rather than a clarity spec alone. Soda-lime cover glass expands near 9 ppm per degree Celsius, thin LCD cell glass sits closer to 3.7 ppm, and polarizer films stretch several times faster. Acrylic optical clear adhesives can exceed 100 ppm, and displacement across a 300-millimeter panel during an 80-degree swing reaches a few tenths of a millimeter, far more than bond line thickness. Once laminated, the softest layer absorbs that difference, and when its modulus is too high, strain migrates to glass edges, polarizer borders, and the brittle indium oxide traces of the touch sensor. The failure is not weak adhesion but stress the geometry cannot relieve.
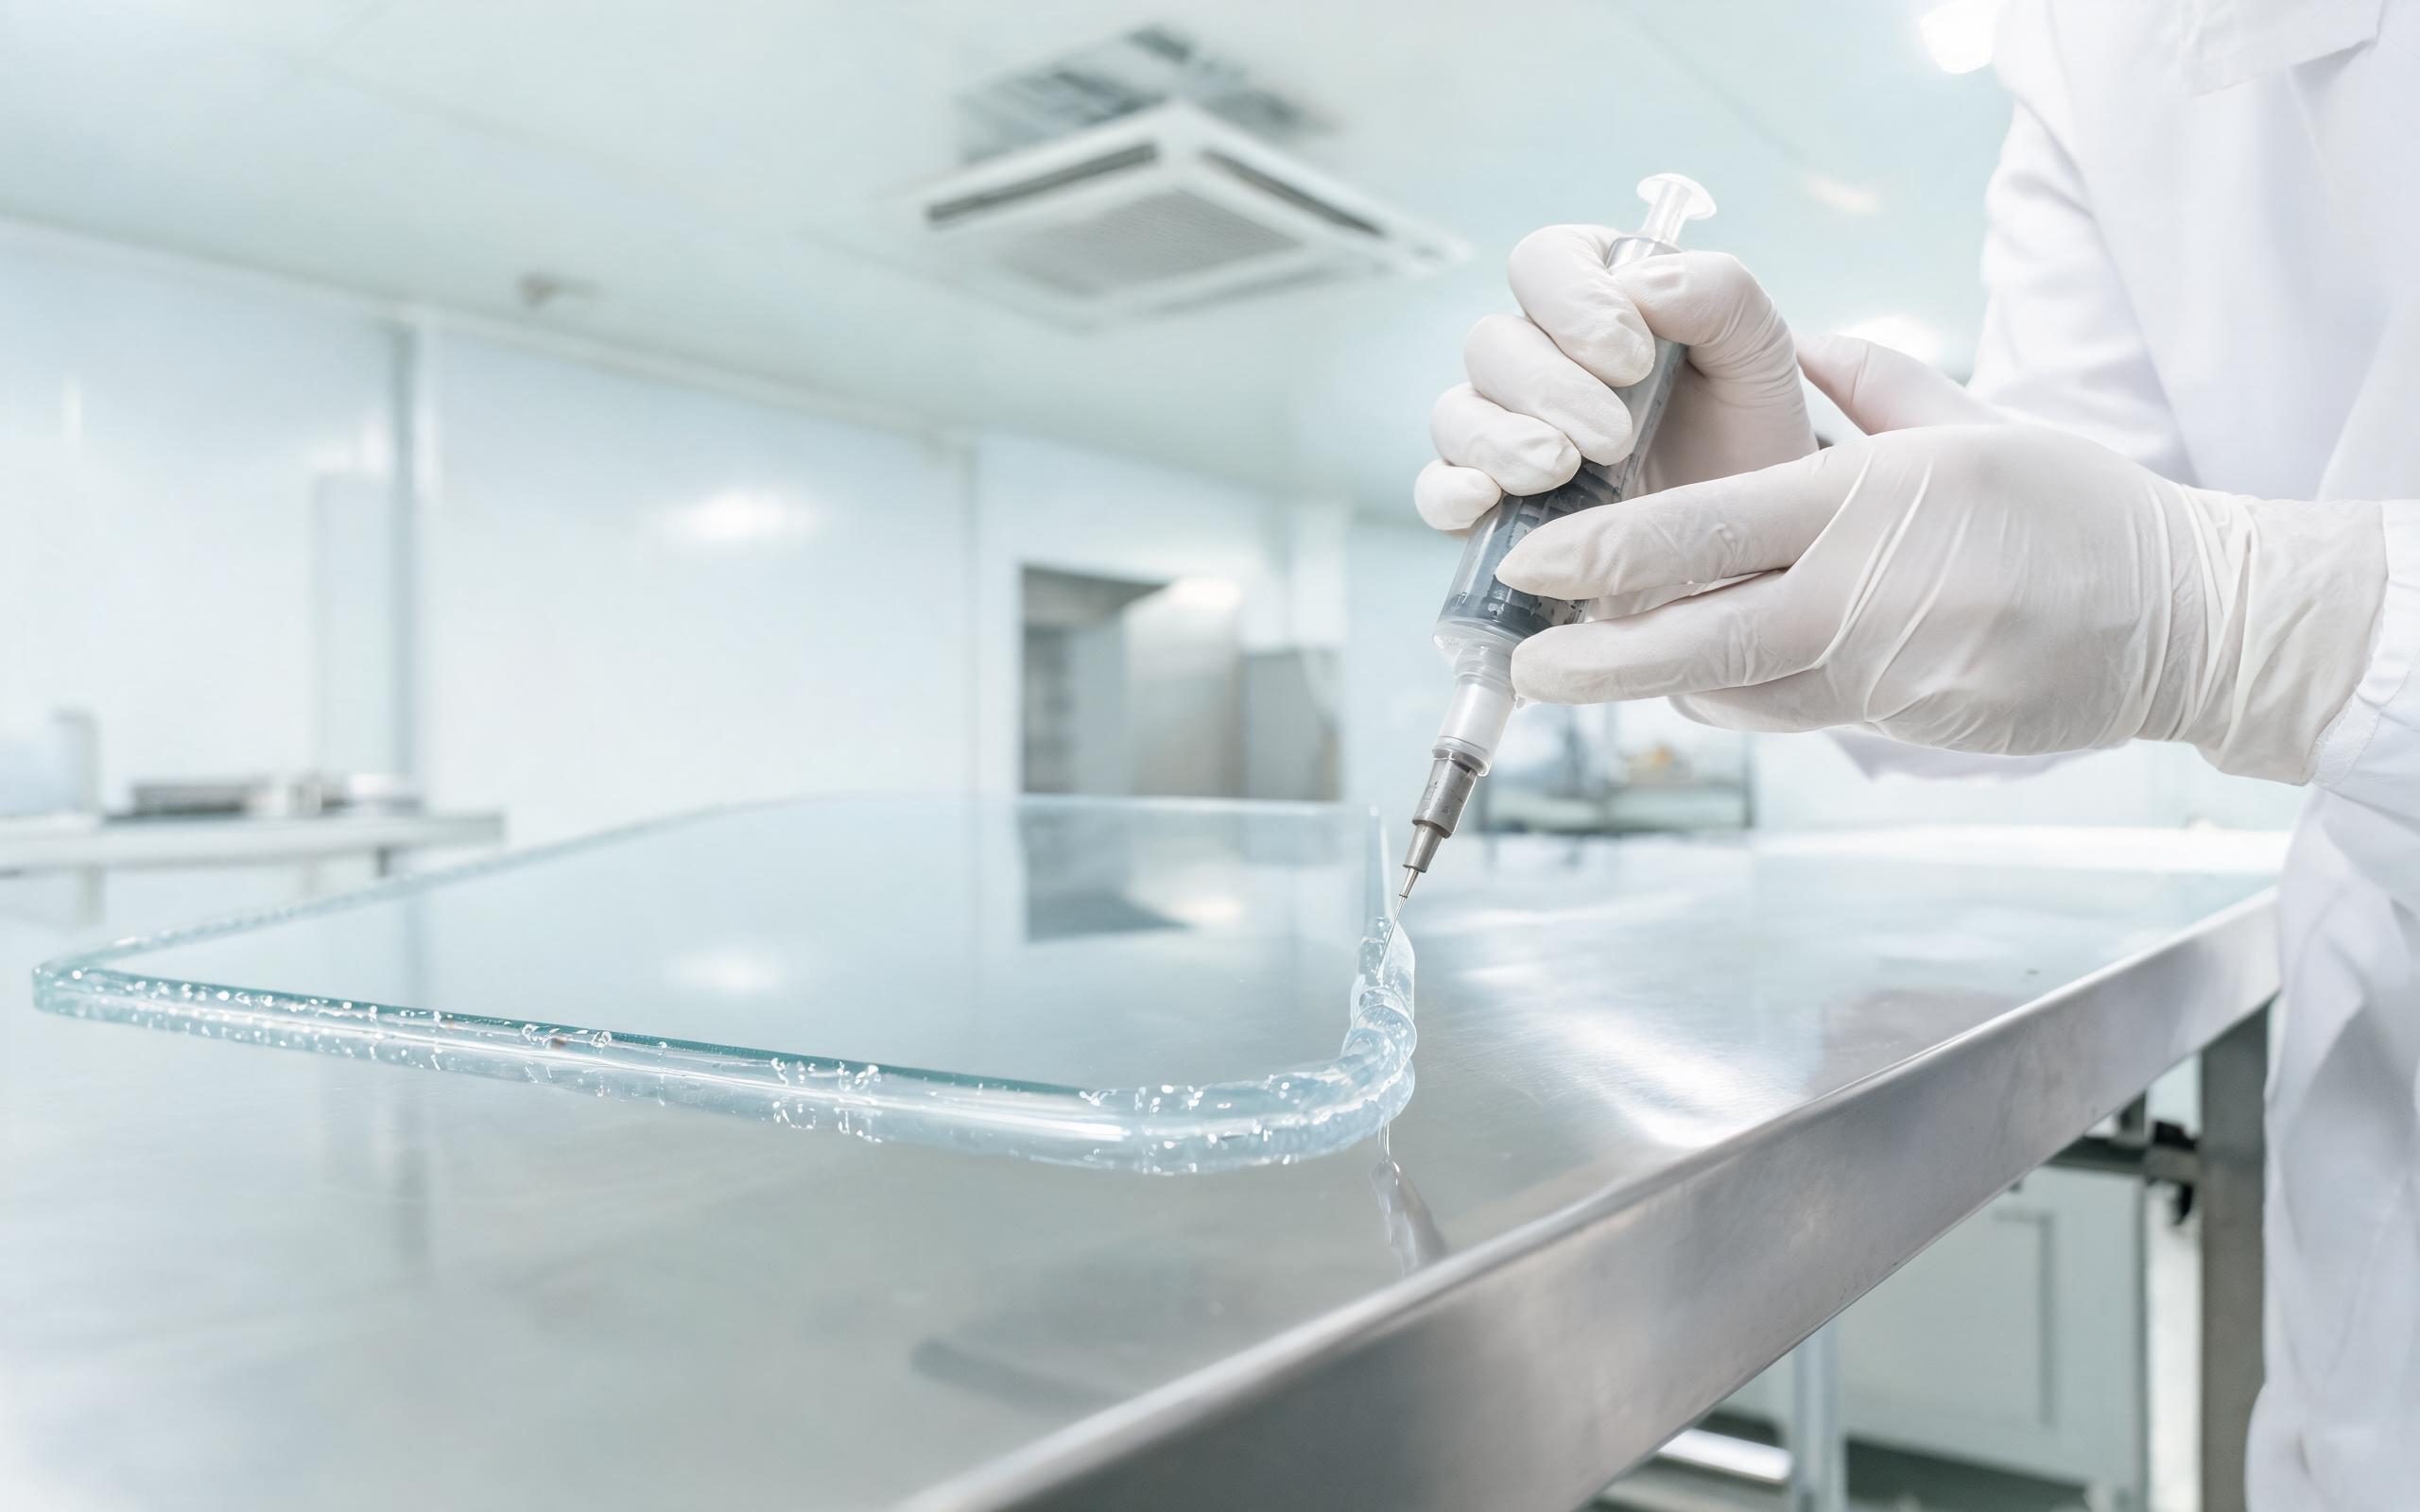
Low-Modulus Adhesives and Edge Strain Relief
Two adhesive families dominate the sealed stack. Rigid acrylic film offers high transparency and fast lamination but a relatively high storage modulus, so it transfers shear toward panel edges outside the comfort range of an office-rated unit. Silicone gel, cured as a liquid optical clear resin, takes a lower modulus and deforms in place, and that compliance keeps a wide temperature panel pc readable through seasonal swings. Geometry shares the work: a dam-and-fill perimeter bead confines the gel behind a narrow free border, while a rounded fillet spreads strain that a square shoulder would concentrate. The staged approach used in the KOXIAN G1 series optical assembly pairs a barrier with a softer center fill and staged ultraviolet cure, releasing shrinkage stress between passes. A ground cover-glass edge stops microcracks from becoming stress risers at the boundary the bond loads most.
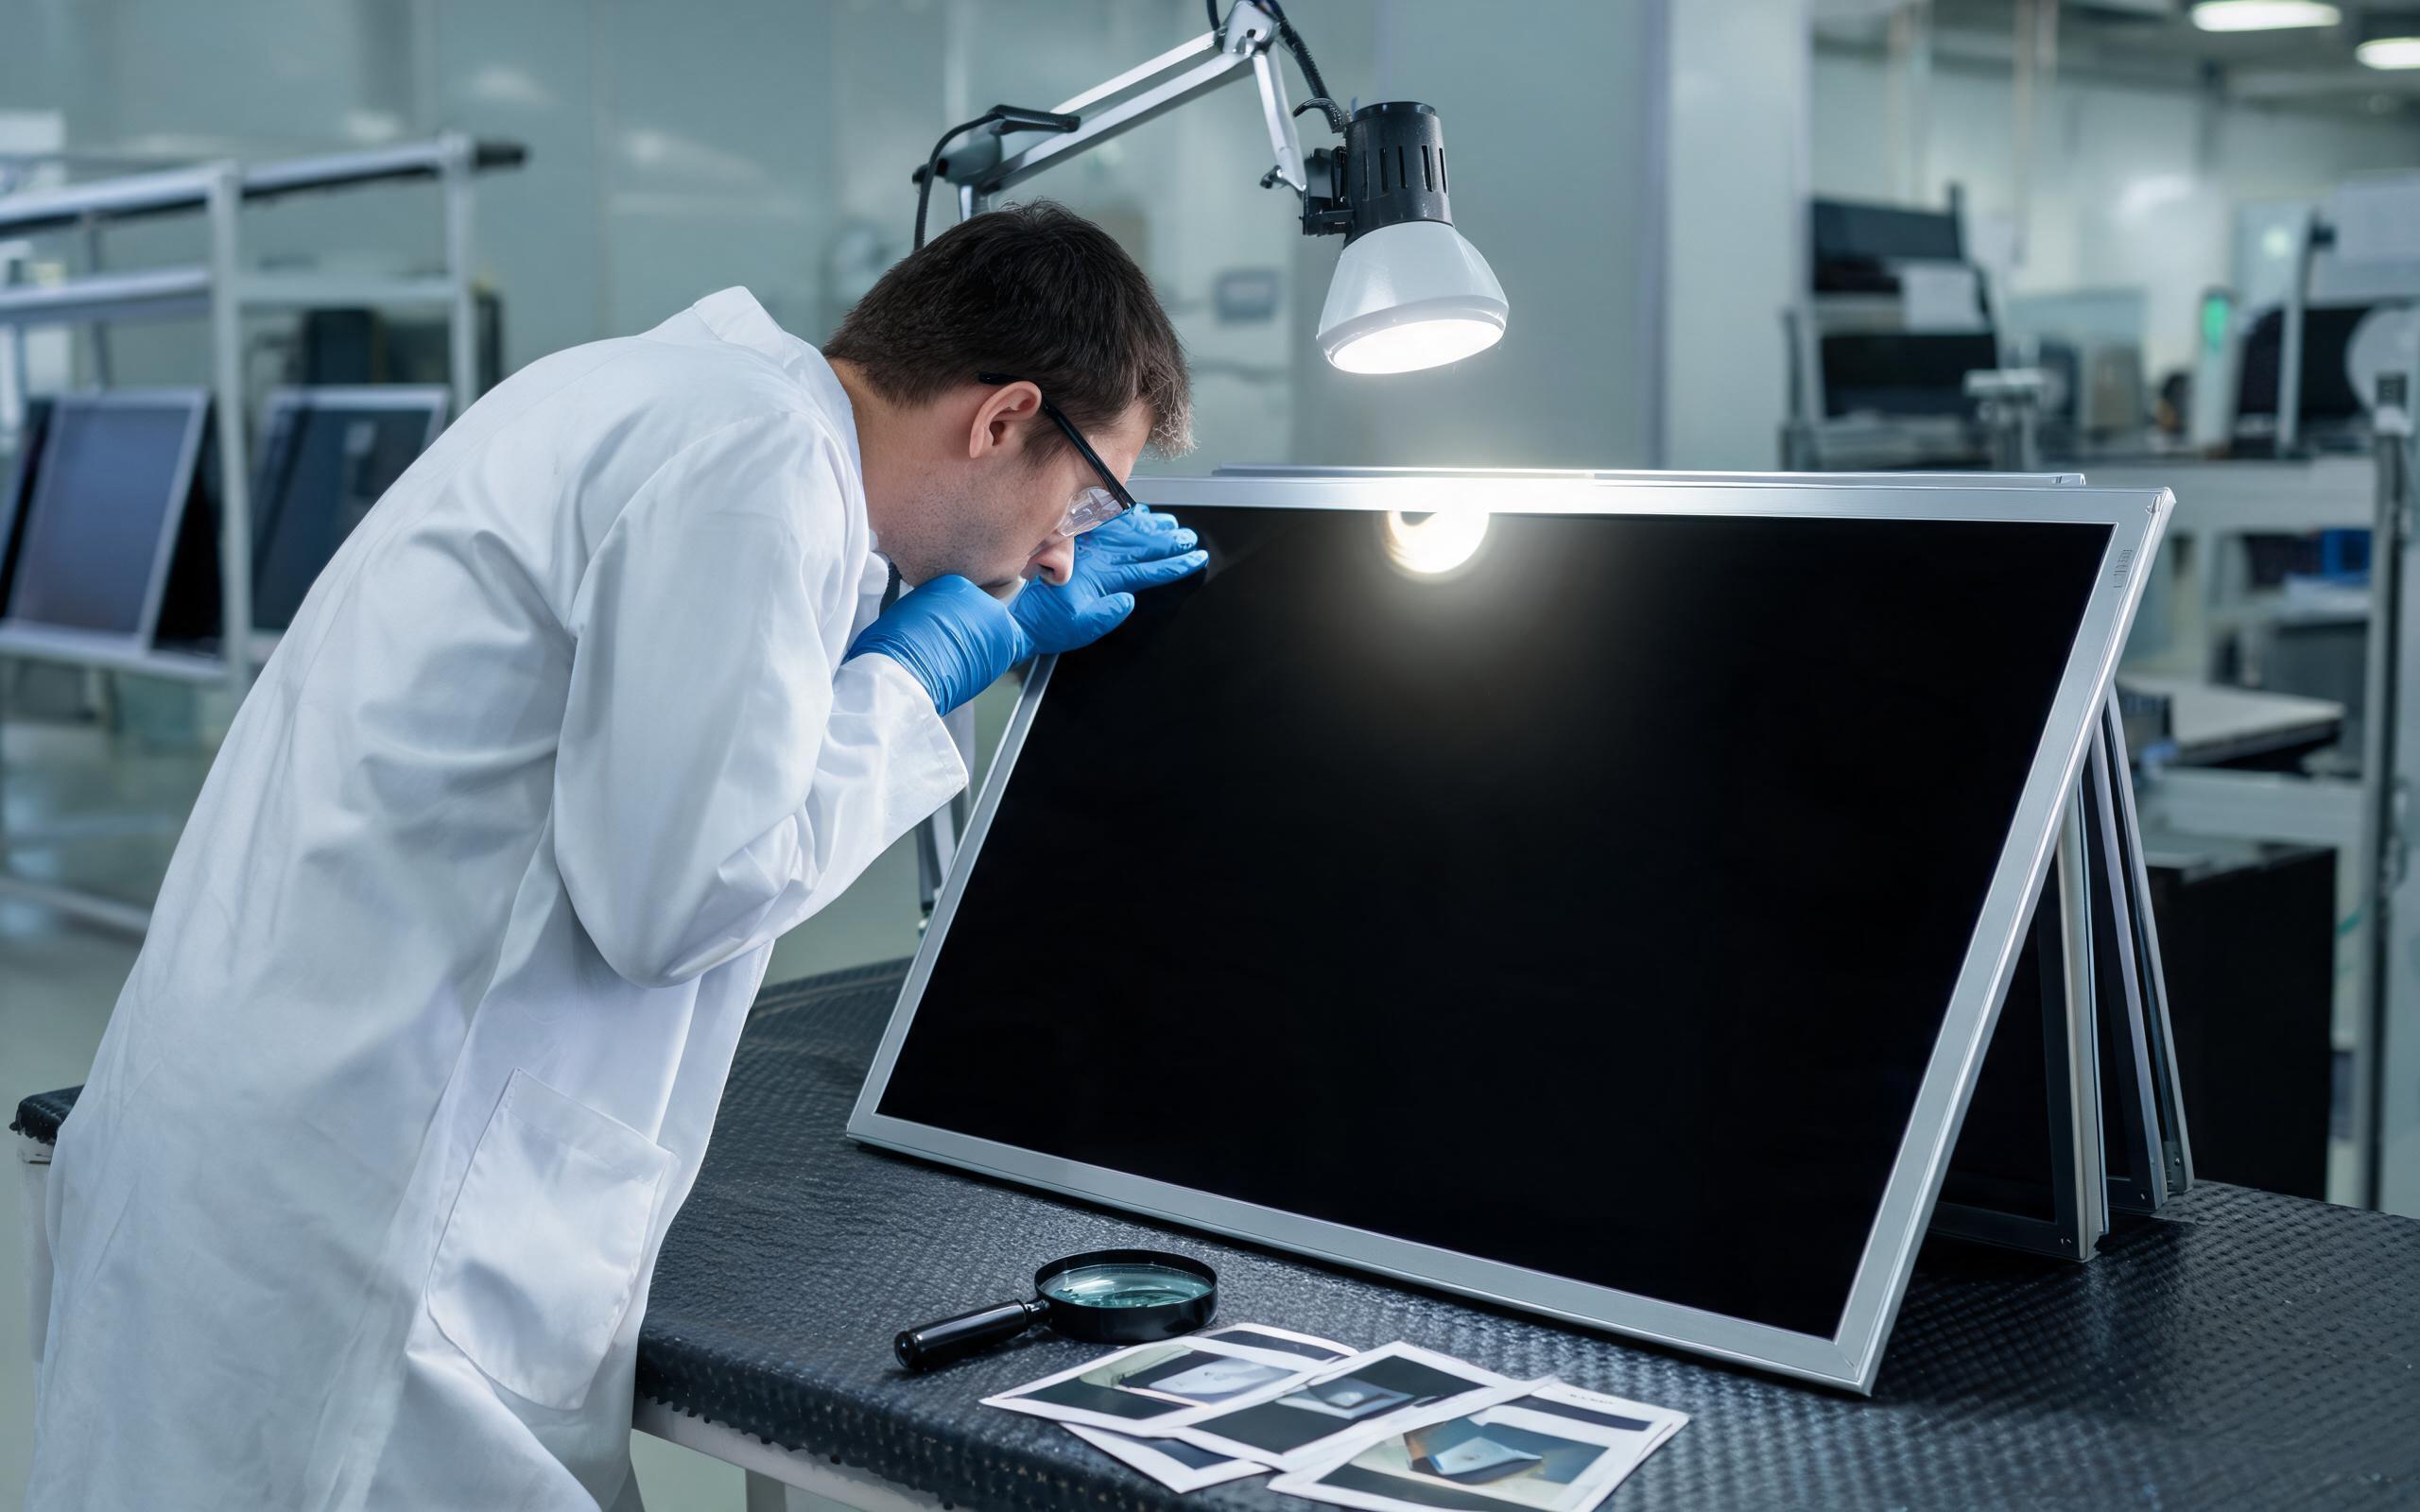
Why Edge Defects Start at Corners and Bezel Lips
Stress does not distribute evenly in a laminated rectangle. The center moves almost freely, but the perimeter is constrained by seal, bezel, and adhesive edge profile, so contraction piles up where two constrained edges meet. Inspectors tracing industrial panel pc optical bonding failures after thermal shock find one sequence: a local halo at a corner, a crescent bubble along the long edge, then a wrinkled polarizer band as the film buckles. The crescent marks a zone where the gel has debonded and reopened a microscopic air cavity, which appears bright against the dark LCD state. Projected-capacitive sensors can survive mild edge lift, but rigid stacks have opened micro-cracks in conductive traces when peel reaches the active area. Once a corner cavity opens, daily cycling pumps moist air in and out, turning a mechanical defect into a fogging defect.
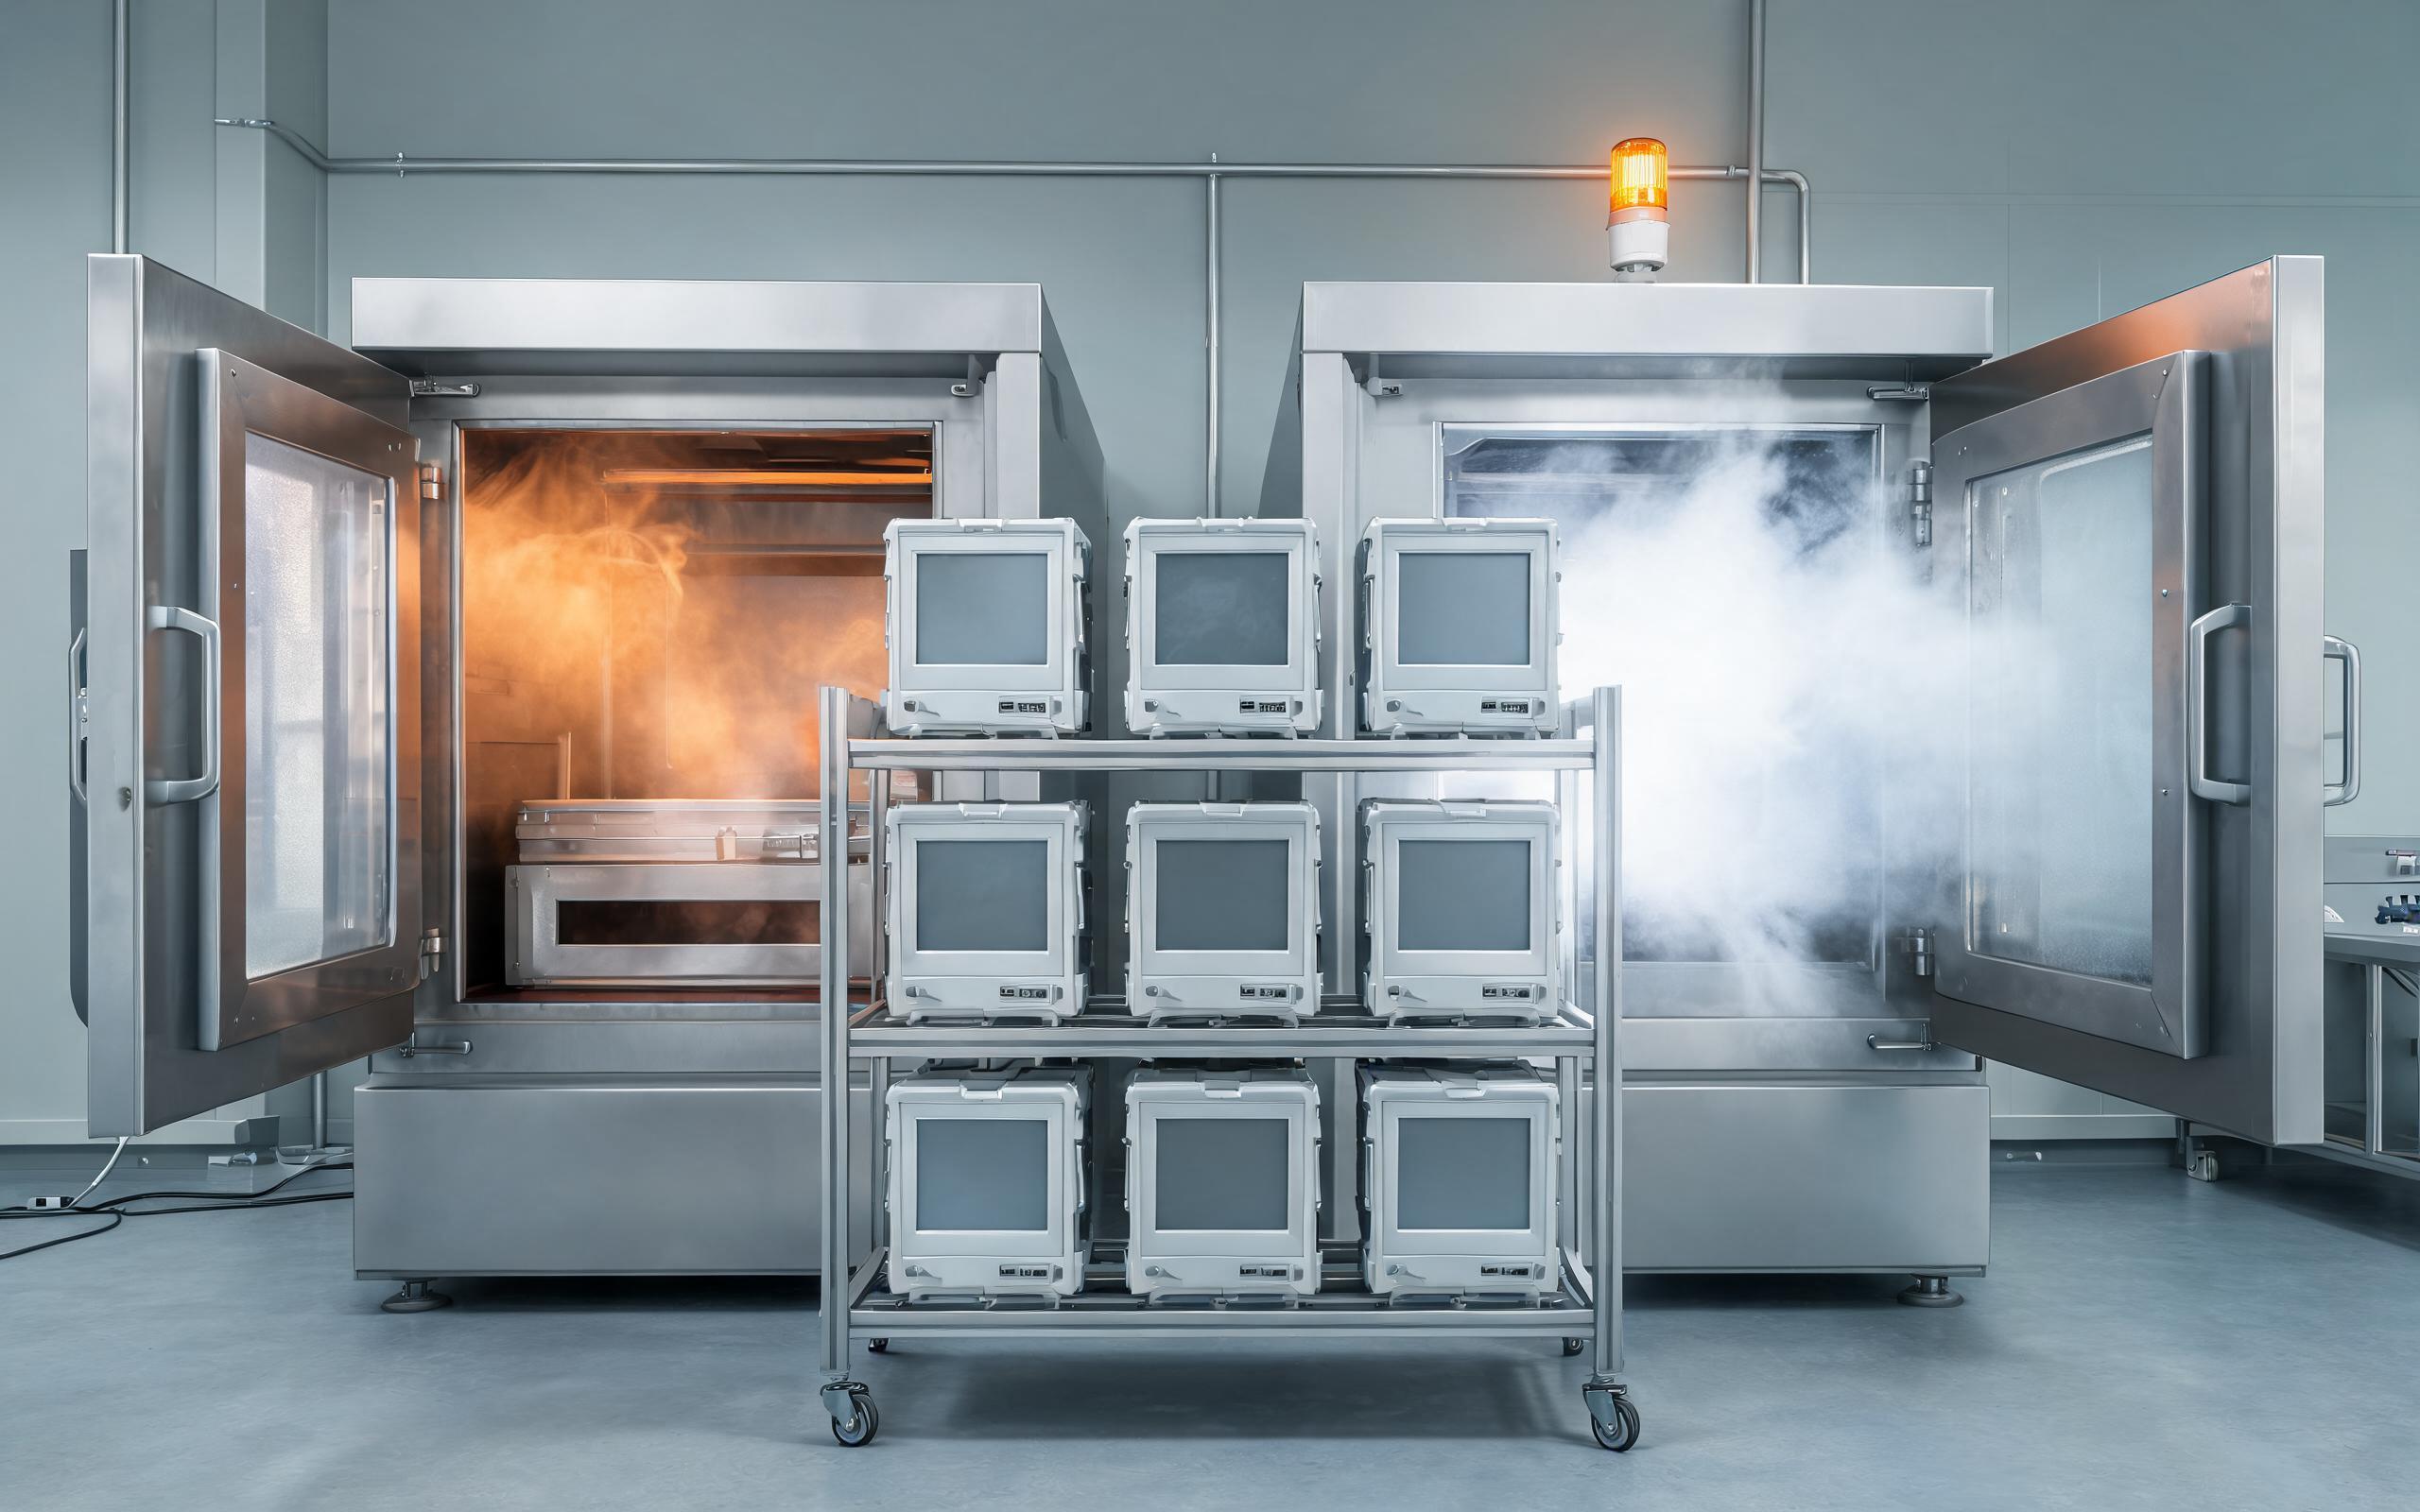
Qualification Cycles for Extreme Temperature Transitions
A rugged industrial display built through industrial panel pc optical bonding earns its label on the chamber floor, not in a datasheet table. Thermal shock qualification follows IEC 60068-2-14 practice, moving assembled units between hot and cold chambers with transitions measured in minutes; a common profile spans minus 40 to plus 85 degrees Celsius with 30-minute dwells and 100 or more cycles. Acceptance goes beyond power-on: inspectors examine edges under polarized light, compare the bond line to reference photographs, run a full touch-grid trace, and re-check the front seal. The panel must pass in its shipping bezel and gasket stack, and qualification repeats after any cover or adhesive change. Chamber testing of KOXIAN-bonded assemblies links each observed edge halo to its originating cycle and confirms whether the free border and gel modulus were sized correctly.
Sealing the air gap solves condensation and dust, but it converts independent layers into one constrained mechanical system. The crescents that arrive with winter cold are expansion-rate problems before they become seal problems. Matching adhesive modulus to the temperature range, leaving a free border with a rounded fillet, and validating the full bezel assembly through chamber cycling keeps bonding an asset rather than a failure mode. Teams comparing wide temperature panel pc and rugged industrial display options should ask for profile, cycle count, and edge-inspection criteria rather than a bonding label.









